Roll family 03 · Intermediate · finishing
Double Poured Indefinite Chill Rolls
Duplex double-pour casting: hard shell, tough core.
About this roll
Indefinite chill rolls: the material
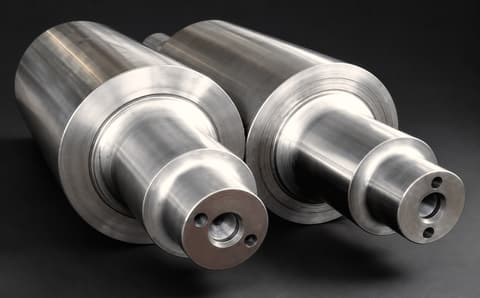
A highly alloyed centrifuged shell as the working layer over a core of grey iron or SG iron, depending on mill requirements. The shell microstructure — carbide and graphite in a matrix progressing from pearlite and bainite through to martensite in harder grades — gives wear resistance controlled by proper dispersion of graphite and carbides. Compared to statically cast double poured rolls: less average hardness drop, a more uniform compact shell, and lower core alloy content imparting higher toughness.
Where it works
Its place in the mill
-
Roughing: not usual here
Heavy passes, high loads
-
Intermediate: used here
Shape and size take form
-
Finishing: used here
Final size and surface
Metallurgy
Composition and properties
Ranges from our grade sheets. The exact composition is set for each order.
| Grade | C % | Si % | Mn % | Cr % | Ni % | Mo % | U.T.S. kg/mm² | Elong. % | Shore C (HSC) |
|---|---|---|---|---|---|---|---|---|---|
| Indefinite Chill | 3.00-3.50 | 0.80-1.50 | 0.55-1.20 | 0.80-1.40 | 1.45-2.50 | 0.25-0.45 | 20-30 | 0.20-0.25 | 55-75 |
| DP Shell — Grade I | 3.15-3.40 | 0.80-1.20 | 0.50-1.00 | 1.30-1.60 | 0.50-4.10 | 0.25-0.40 | — | — | 70-75 |
| DP Shell — Grade II | 3.20-3.45 | 0.80-1.20 | 0.60-1.00 | 1.30-1.70 | 3.00-4.25 | 0.25-0.40 | — | — | 75-80 |
| DP Shell — Grade III | 3.30-3.50 | 0.80-1.20 | 0.65-1.10 | 1.40-2.00 | 3.50-4.50 | 0.25-0.40 | — | — | 80-85 |
| GI Core (double pour) | 3.00-3.50 | 1.50-2.50 | 0.45-0.60 | 0.60 Max | — | — | 20-30 | 0.20-0.25 | 35-45 |
| SG Core (double pour) | 3.00-3.40 | 1.90-2.70 | 0.50 Max | 0.60 Max | — | — | 35-50 | 0.50-0.65 | 35-45 |
- Alloy cast steel 30–45
- Grey iron core 35–45
- SG iron core 35–45
- Adamite steel base 45–55
- SG pearlitic 45–55
- SG pearlitic (hard) 55–65
- Definite chill 55–70
- Indefinite chill 55–75
- SG acicular 65–75
- Non metal 65–75
- Definite chill (hard) 70–75
- DP shell I 70–75
- SG acicular (hard) 75–80
- DP shell II 75–80
- HSS I 75–80
- HSS II 75–80
- DP shell III 80–85
Recommended use
Where we recommend it
Mills and stands where this roll is the usual choice, with the barrel hardness we recommend.
| Rolled product | Type of mill | Stand and barrel hardness, Shore C |
|---|---|---|
| Flat products for steel mills | ||
| Wide Hot Strip | 4 High Continuous |
|
| Wide Hot Strip | Continuous |
|
| Wide Hot Strip | Finishing Train |
|
| Wide Hot Strip | 4 High Reversing |
|
| Wide Hot Strip | 2 High |
|
| Wide Hot Strip | 4 High |
|
| Cold Strip | 4 High Reduction |
|
| Cold Strip | 4 Temper |
|
| Plates | 2 High |
|
| Plates | 3 High |
|
| Plates | 4 High |
|
| Sheet | 2 & 3 High |
|
| Shaped products for steel mills | ||
| Billets, Bars & Round | 2 & 3 High |
|
| Medium Sections | 2 & 3 High |
|
| Light Section Bar | 2 & 3 High |
|
| Billets | Continuous |
|
| Medium & Light Sections | Continuous |
|
| Wire Rod | Continuous |
|
| Rolls for non-ferrous metals | ||
| Slabs | 4 High Finish |
|
| Shaped Products | 2 High |
|
Production process
From melt to mill
Centrifugal cast rolls
A double-poured sleeve, shrink-fitted onto a steel shaft.
-
Charge mix
Tested scrap, pig iron and alloys, weighed to the grade.
-
Melting
The melt is analysed and balanced to the grade's chemistry.
-
Centrifugal casting
Double pour in a spinning mould: a hard shell, then a tough inner layer.
-
Heat treatment
Hardening and tempering on a controlled temperature cycle.
-
Proof machining
A first cut shows that the metal is sound.
-
Shrink fit
The heated sleeve grips the shaft as it cools.
-
Necks & grooves
Necks, faces and pass grooves cut to the mill's drawing.
-
Grinding
A final grind brings the barrel to size and finish.
-
Testing
Hardness, soundness and balance checked before release.
-
Certificate & dispatch
Packed with its test certificate, for India and abroad.
- Your roll drawing, or barrel and neck sizes
- Mill type and the stand for the roll
- Material rolled and the pass or groove
- Quantity and the date you need it
Our range
Other roll families
- 01 Clear chill rolls Finishing stands
- 02 Alloy cast steel rolls Roughing stands
- 04 Adamite rolls Roughing · section mills
- 05 Multi rolls Mixed schedules
- 06 Forged rolls Cold rolling · high duty
- 07 SG iron rolls Roughing · intermediate
- 08 SGACC rolls Intermediate · finishing
- 09 HSS rolls Intermediate · finishing
- 10 Metal rolls General applications
Need this roll for your mill?
Send your drawing or roll size — we will quote by return.