Roll family 08 · Intermediate · finishing
SG Acicular Rolls (SGACC)
Acicular SG structure for superior wear performance.
About this roll
SGACC rolls: the material
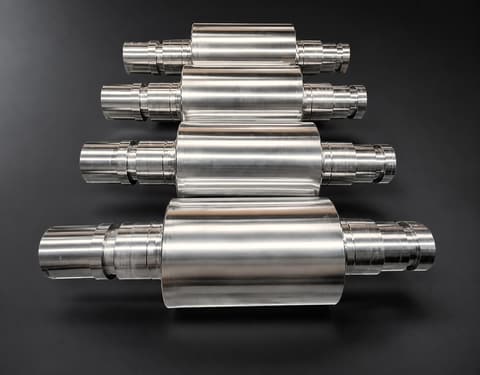
Nodular acicular rolls widely used for hot rolling in intermediate, prefinishing and finishing group stands. The material consists of nodular graphite and carbides in a martensitic and bainitic matrix — more wear resistant than nodular pearlitic rolls. Standard and higher-alloyed variants are chosen per mill conditions, where wear resistance increases with hardness drop against standard grades for the type of groove or calibre.
Where it works
Its place in the mill
-
Roughing: not usual here
Heavy passes, high loads
-
Intermediate: used here
Shape and size take form
-
Finishing: used here
Final size and surface
Metallurgy
Composition and properties
Ranges from our grade sheets. The exact composition is set for each order.
| Grade | C % | Si % | Mn % | Cr % | Ni % | Mo % | U.T.S. kg/mm² | Elong. % | Shore C (HSC) |
|---|---|---|---|---|---|---|---|---|---|
| SG Iron — Acicular | 3.20-3.50 | 1.20-1.70 | 0.50-0.70 | 0.30-0.70 | 2.00-3.00 | 0.70-1.10 | 40-65 | 1.00-2.00 | 65-75 |
| SG Iron — Acicular (hard) | 3.25-3.55 | 1.20-1.50 | 0.50-0.70 | 0.30-0.80 | 2.80-4.00 | 0.70-1.20 | 40-65 | 1.00-2.00 | 75-80 |
- Alloy cast steel 30–45
- Grey iron core 35–45
- SG iron core 35–45
- Adamite steel base 45–55
- SG pearlitic 45–55
- SG pearlitic (hard) 55–65
- Definite chill 55–70
- Indefinite chill 55–75
- SG acicular 65–75
- Non metal 65–75
- Definite chill (hard) 70–75
- DP shell I 70–75
- SG acicular (hard) 75–80
- DP shell II 75–80
- HSS I 75–80
- HSS II 75–80
- DP shell III 80–85
Recommended use
Where we recommend it
Mills and stands where this roll is the usual choice, with the barrel hardness we recommend.
| Rolled product | Type of mill | Stand and barrel hardness, Shore C |
|---|---|---|
| Flat products for steel mills | ||
| Plates | 2 High |
|
| Plates | 4 High |
|
| Sheet | 2 & 3 High |
|
| Shaped products for steel mills | ||
| Medium Sections | 2 & 3 High |
|
| Light Section Bar | 2 & 3 High |
|
| Medium & Light Sections | Continuous |
|
| Wire Rod | Continuous |
|
| Rolls for non-ferrous metals | ||
| Slabs | 4 High Finish |
|
| Shaped Products | 2 High |
|
Production process
From melt to mill
Static cast rolls
Cast in one piece in a chill mould.
-
Charge mix
Pig iron and foundry returns, weighed for each heat.
-
Melting
Tapped into the ladle once the chemistry is right.
-
Static casting
Poured into a chill mould that freezes a hard working face.
-
Heat treatment
Hardening and tempering on a controlled temperature cycle.
-
Rough machining
Barrel and necks turned close to size.
-
Necks & wobblers
Necks, faces and wobblers shaped to the mill's drawing.
-
Grinding
A final grind brings the barrel to size and finish.
-
Testing
Shore hardness mapped across the barrel.
-
Certificate & dispatch
Rested on timber saddles and strapped, with its certificate.
- Your roll drawing, or barrel and neck sizes
- Mill type and the stand for the roll
- Material rolled and the pass or groove
- Quantity and the date you need it
Our range
Other roll families
- 01 Clear chill rolls Finishing stands
- 02 Alloy cast steel rolls Roughing stands
- 03 Indefinite chill rolls Intermediate · finishing
- 04 Adamite rolls Roughing · section mills
- 05 Multi rolls Mixed schedules
- 06 Forged rolls Cold rolling · high duty
- 07 SG iron rolls Roughing · intermediate
- 09 HSS rolls Intermediate · finishing
- 10 Metal rolls General applications
Need this roll for your mill?
Send your drawing or roll size — we will quote by return.